How to Specify a Non Woven Bag Printing Machine: Servo, PLC and Seal Parameters
Short answer: a non woven bag printing machine should be specified by (1) its drive and control tier — servo drive with encoder feedback and a named PLC brand; (2) its integration level — a fully automatic inline flow running 100–120 pcs/min against 15–20 pcs/min for semi-automatic lines; and (3) its sealing reliability — accepted with a pull test in which the seal tears the fabric instead of peeling, against a defect target below 0.5%.
Introduction: The Brief Is Not the Specification
A non woven bag printing machine is normally bought against a short brief: flexo, four colors, 1,200 mm roll width. That brief is also where most of the value is lost, because two machines that match it exactly can still differ substantially in output speed, seal consistency and unattended running hours. The specification that decides those outcomes sits in three places a quotation often leaves blank — the drive and control tier (servo motor, PLC and HMI), the integration level (a standalone printer or a fully integrated inline flow from feeding to stacking), and sealing reliability (ultrasonic or heat-seal parameters plus the acceptance criteria applied at pre-shipment test).
This guide is written for importers, bag factory owners, OEM buyers and procurement engineers who are close to issuing a purchase order for a non woven bag printing machine, or who are configuring printing capacity alongside a bag making line. It explains how to write each of the three layers into a specification, how to test what you bought before the balance payment, what preventive maintenance the servo, PLC and sealing systems require, and which purchasing terms should be confirmed in writing before the order is placed.
Problem Definition: Why Two Identical-Looking Machines Deliver Different Results
Selection risk does not start at the port; it starts at the quotation stage, where three items are commonly left undefined and later become quality disputes.
Gap 1 — the drive and control tier is described with generic words
Terms such as “servo motor” or “PLC control” are not specifications. A closed-loop servo system carries an encoder that reports actual position to the drive, which compares target and actual values and corrects the error in real time. That is why a servo-driven machine holds bag length to ±0.5 mm at 120 bags per minute, while an open-loop clutch drive drifts by ±2–3 mm as belts wear and voltage fluctuates. For supermarket supply, where bag size consistency is an incoming-inspection condition, that difference decides whether a delivery is accepted.
Gap 2 — printing is purchased as a standalone step instead of an integrated flow
A standalone printer produces printed roll stock that must be rewound, stored, moved and re-fed into a separate bag line. An integrated inline flow runs feeding → printing → forming → sealing → cutting → counting → stacking with no manual transfer between stations. Integration is not a presentation preference; it changes operator count, floor layout, handling damage and the achievable defect rate. It also changes the specification question from “which printer” to “which printer can sustain the bag line’s demand without becoming the constraint”.
Gap 3 — sealing method and acceptance criteria are not written into the contract
Weak or inconsistent bag seals are the most common quality issue in non-woven bag production, and they are usually a setup and verification problem rather than a machine defect. Three root causes cover roughly 90% of cases: ultrasonic horn surfaces contaminated with melted fabric residue; an incorrect or uneven horn-to-anvil gap; and an amplitude or speed mismatch after a fabric GSM change. All three are avoidable — but only if the sealing method, the sealing parameters and the acceptance test are written into the order and verified at pre-shipment test rather than discovered after the container is unloaded.
Industry Background: Why Specification Depth Now Decides Competitiveness
The demand context behind non-woven bag printing investment is regulatory and structural rather than cyclical:
- More than 100 countries have implemented bans or taxes on single-use plastic bags, which drives conversion to reusable non-woven formats.
- Global production of non-woven bags exceeded 58 billion units in 2023.
- The global market for nonwoven fabrics used in packaging is estimated at USD 6.34 billion in 2026.
- The global non-woven bag making machine market is projected to grow from USD 179 million in 2025 to USD 733 million by 2032, according to LP Information, a CAGR of 22.5% from 2026 to 2032.
- Asia-Pacific held a 43.6% revenue share of the bag making machine market in 2025 (Dataintelo).
- Automatic machines accounted for 52.4% of the bag making machine market in 2025.
- The global flexographic printing machine market was valued at USD 17.57 billion in 2024, with a projected CAGR of 9.7% through 2030 (Grand View Research).
- The average price for an automated non-woven bag making machine in 2025 was approximately USD 29,000 (LP Information).
The practical reading of these numbers is straightforward. The market has already shifted to automatic platforms, and automatic platforms hold the majority share. What separates one quotation from another is therefore no longer “automatic versus manual” — it is how precisely the drive tier, the integration level and the sealing reliability are defined inside an automatic platform, because those three choices determine output per shift, operator headcount, scrap volume and the maintenance workload the buyer inherits.
Detailed Solution: The Three Specification Layers
Layer 1 — Drive and control tier: servo motor, PLC and HMI
A servo motor is a precision electric motor with a built-in position sensor (encoder) that reports its exact rotational angle back to a controller thousands of times per second. In a bag machine, the servo drives the fabric feeding rollers, and the encoder confirms that the commanded rotation was actually completed — if the encoder reports a shortfall, the drive applies additional current to complete the remaining movement before the error accumulates into a dimensional defect.
- Servo system composition: a permanent-magnet servo motor with low rotor inertia, an encoder with 17-bit to 20-bit resolution (131,072 to 1,048,576 positions per revolution), and a servo drive that corrects position and velocity error every 125–250 microseconds.
- Accuracy outcome: ±0.5 mm bag dimensional accuracy at production speeds up to 120 bags per minute, versus typical ±2–3 mm drift on open-loop drive systems.
- Energy outcome: 25–30% lower total energy consumption than a constant-speed clutch motor, because current is drawn mainly during acceleration and working phases rather than continuously.
The PLC is the controller that executes the machine program: it reads sensor, limit-switch and photocell inputs, applies logic, and updates motor, valve and alarm outputs in a continuous scan cycle measured in milliseconds. The HMI touch screen is the operator layer — it displays speed, count and fault messages, and stores complete machine setups as recipes, so a bag change becomes a one-touch recall of feeding length, sealing time, cutting position, speed limit and photocell offset.
Component brand is a legitimate specification item, not a preference. Machines can be built with Siemens, Delta or Mitsubishi PLCs, Omron sensors and NSK bearings, and those components can be verified by third-party inspection — SGS, Bureau Veritas or CCIC — at the buyer’s request before shipment. When a supplier cannot name the PLC series or accept third-party verification, the drive tier is effectively unspecified.
What to write into the purchase order for Layer 1: servo drive with encoder feedback rather than a clutch drive; PLC brand and series; HMI language and recipe storage; sensor and bearing brands; motor brand options; and the acceptance of a third-party pre-shipment inspection.
Layer 2 — Integration level: standalone printer or fully integrated inline flow
Integration level defines the number of times material is handled between printing and the finished bag. In a fully integrated inline flow the sequence is continuous: feeding → printing → forming → sealing → cutting → counting → stacking. There is no rewind, no intermediate storage and no manual transfer between stations.
The measurable difference between the two automation tiers is documented in the equipment data:
- Fully automatic inline: 100–120 pcs/min, one operator per two machines, integrated inline process, defect rate below 0.5%, PLC self-diagnosis supporting preventive maintenance.
- Semi-automatic: 15–20 pcs/min, three to four workers per line, separate stations with manual material transfer between processes, and a defect rate in the 3–5% range.
At 100 pcs/min and a realistic 85% uptime, an eight-hour shift produces roughly 40,800 bags; planning at rated speed without an uptime discount is where capacity projections usually fail. Semi-automatic lines make sense for capital-constrained startups below approximately 10,000 bags per day, or for production dominated by very small custom batches where changeover time outweighs the automation speed advantage.
On the printing side, the machine class determines where the printing unit sits in the flow and how fast it can feed it:
- ZXH-A1200 — one-color screen printing, printing speed 1,500–4,000 m/hour.
- ZXH-B1200 — two-color screen printing, printing speed 1,500–3,000 m/hour.
- ZXH-C21200 — two-color flexo printing, 10–60 m/min.
- ZXH-C41200 — four-color flexo printing, 10–60 m/min.
Flexographic configurations can be customized from 1 to 6 colors. The decision rule for integration is the speed envelope: the printing unit must be able to sustain the bag line’s demand at the required color count, or it becomes the bottleneck and the inline advantage disappears. A second, practical rule comes from how buyers sequence investment: if confirmed printing orders do not yet exist, plain bags can be sold to customers who apply stickers or heat-transfer labels, and the printing unit added later when demand is proven.
Layer 3 — Sealing reliability: method, parameters and acceptance
Ultrasonic welding converts 20 kHz electrical energy into mechanical vibration through a transducer and a horn, creating friction heat at the interface between fabric layers. The melt zone is confined to approximately 0.1–0.3 mm at the contact interface and forms within 0.2–0.5 seconds, so the outer fabric surface stays cool and undamaged. Compared with heat sealing, the practical differences are: 15–20% higher peel strength, 25–30% lower energy consumption, no 15–20 minute warm-up, and no consumables other than the horn itself, which typically wears out on a 12–18 month cycle. Heat sealing at 180–220°C transfers heat through the full fabric thickness, which risks scorching and odor, and requires heating element replacement every 3–6 months. Ultrasonic is the required method where odor-free, clean seals matter — food takeaway bags, for example — while heat sealing remains acceptable for basic non-food shopping bags.
Once the method is fixed, three parameters must be specified and recorded as recipes:
| Fabric GSM | Amplitude setting | Setting notes |
|---|---|---|
| 50–60 GSM | 60–70% | Thin fabric needs lower welding energy; check for incomplete fusion before increasing amplitude. |
| 70–90 GSM | 75–85% | Standard shopping bag range. Horn-to-anvil gap approximately 0.3–0.5 mm, even within 0.05 mm across the full horn width. |
| 100–150 GSM | 90–100% | Thicker or laminated fabric. Verify gap parallelism with a feeler gauge at both horn ends before production. |
Amplitude controls welding energy; the horn-to-anvil gap controls compression and must be measured with a feeler gauge at both ends and the center, because an uneven gap produces strong seals on one side and weak seals on the other. Speed is the third variable: increasing production speed shortens weld contact time per bag, so amplitude normally has to be increased to compensate. Print registration is handled separately by a photocell that detects a printed registration mark — typically a 5 × 5 mm black square — against the light fabric, and signals the PLC to time the cut and seal. Marks smaller than 5 mm or printed with faded ink can be missed at production speed. Where premium brand packaging is the target, print registration accuracy is specified at ±0.3 mm.
The acceptance rule that settles disputes: after any parameter change, run 20 test bags and pull-test 5 by hand. A correct seal tears the fabric; an incorrect seal peels apart at the weld line. A uniform, slightly glossy weld line is correct; a brown line or distorted fabric means amplitude is too high.
Step-by-Step Breakdown: From Specification to Acceptance
Step 1 — Fix output target, bag style and material first
Daily output, bag style (D-cut, W-cut, flat, box, gusseted) and fabric GSM range determine the machine tier before any printing question is asked. Thicker fabric runs slower: 100–120 GSM fabric typically runs 10–15% slower than 70 GSM, and multi-color printing reduces line speed relative to unprinted production.
Step 2 — Write the drive and control tier into the order
Name the PLC brand and series, require servo drive with encoder feedback, specify the HMI language, and confirm that third-party inspection (SGS, Bureau Veritas, CCIC) will be permitted before shipment.
Step 3 — Choose the integration level and the printing type
Decide between a fully automatic inline flow and a semi-automatic configuration, then match the printing unit — screen or flexo, in the color count your order book actually requires — to the line’s speed envelope.
Step 4 — Define the sealing method and the seal acceptance criteria
Specify ultrasonic or heat sealing, record amplitude, gap and speed settings per GSM as recipes, and write the pull-test criterion into the contract: 20 test bags produced, 5 pull-tested, seal must tear fabric rather than peel.
Step 5 — Plan the installation before the container ships
Site preparation is the buyer’s responsibility and the most common cause of delayed commissioning. Before the machine arrives: level concrete floor with 1.5 m clearance on all sides; three-phase power installed and verified with a multimeter at the correct voltage; industrial air compressor with dryer and tank installed; voltage stabilizer wired in where grid power fluctuates; and 1–2 tons of PP spunbond fabric (70–80 GSM for initial production) on site. Installation of a standard single machine takes one to two working days — day one for uncrating, positioning, leveling, power and air connection; day two for fabric threading, dry run, first production test, parameter fine-tuning and operator training. Commissioning normally proceeds from a dry run at 20–30 pcs/min to a low-speed fabric run at 30 pcs/min with the first 50 bags inspected, then a ramp to 60, 80 and 100 pcs/min with inspection at each tier. Zhengxin engineers support the process over WhatsApp or video call and more than 90% of installations are completed through remote guidance; on-site engineer dispatch is available at USD 100 per day plus airfare and accommodation if remote support is not sufficient.
Step 6 — Set the preventive maintenance schedule before production starts
Maintenance on a printing and sealing line is short but non-negotiable:
- Daily (5–10 minutes): clean fabric dust from rollers, guide bars and photocell lenses; drain water from the air compressor tank; wipe the ultrasonic horn and anvil with isopropyl alcohol; inspect the fabric path; test emergency stops; listen for new noise in the first minute of operation.
- Weekly (15–20 minutes): grease chain drives, linear rails, lead screws and bearings with the specified grease; check drive belt tension (5–10 mm deflection at the midpoint under moderate finger pressure); check pneumatic hoses for leaks; clean the electrical cabinet air filter; tighten visible fasteners.
- Monthly: clean or replace the compressor intake filter; inspect the ultrasonic horn surface for pitting or uneven wear and replace if the surface is no longer flat; check blade sharpness and replace if edges tear rather than cut; verify guards and interlocks; back up PLC parameters and recipes to USB.
- Quarterly: professional inspection of electrical connections; ultrasonic generator output test; replacement of worn consumables.
Two safety rules belong in the operating procedure from day one: always isolate the main electrical supply before maintenance, because the HMI stop button does not cut all power; and never touch the ultrasonic horn while the generator is powered.
Step 7 — Confirm purchasing terms and acceptance procedure before the order
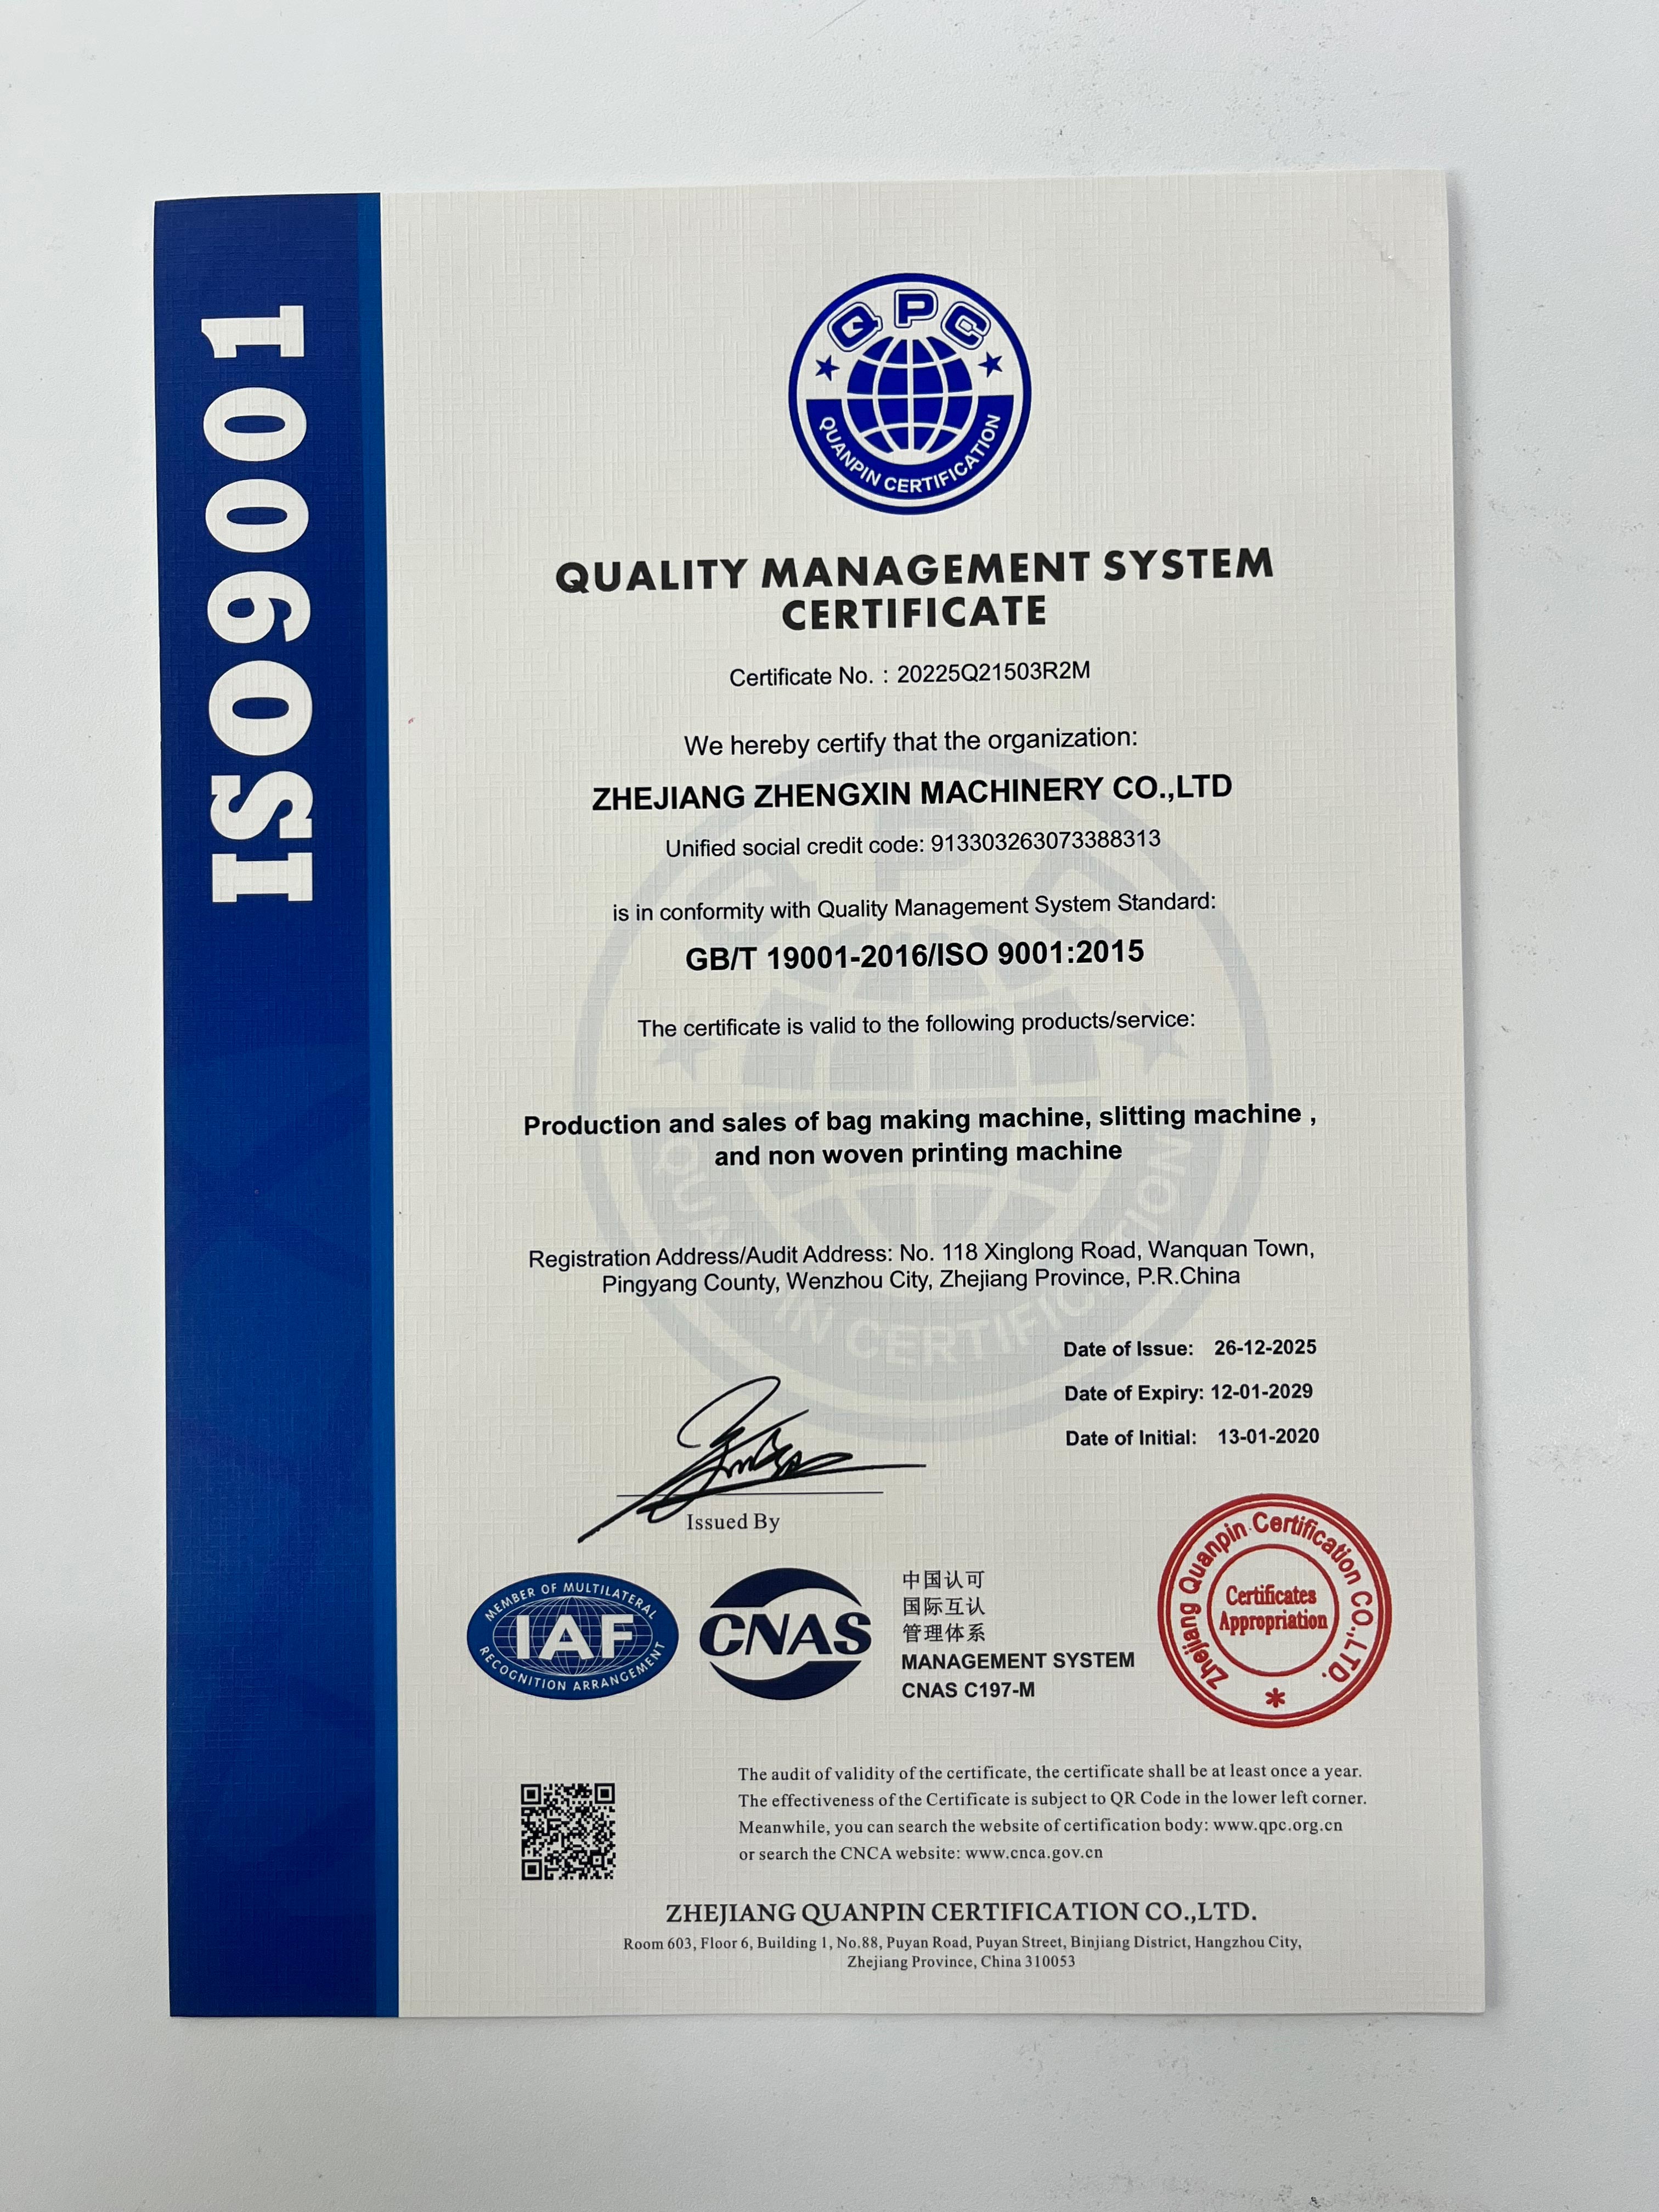
Terms to verify in writing: minimum order quantity of 1 unit; delivery terms FOB or CIF; acceptance criteria defined as pre-shipment testing; payment terms 30% deposit and 70% before shipment. Production lead time is quoted in the 30–45 day range depending on configuration, and sea freight adds 15–45 days depending on destination, so total order-to-port timing should be planned rather than assumed. Zhengxin supplies ISO 9001:2015 and CE documentation with the machine, and country-specific certification such as SONCAP, PVOC or SASO can be arranged on request.
Use Cases: How the Three Layers Play Out in Real Installations
The specification logic above is not theoretical — it shows up in how buyers configure printing capacity in different markets.
- Egypt — food packaging and retail shopping bag manufacturer. Five units (ZXL-E700 ×1, ZXH-C21200 ×2, ZXL-D700 ×2) support two distinct product lines: food takeaway bags for restaurant chains and delivery platforms, and multi-color printed promotional shopping bags for retail malls. Running since 2017, the configuration established the company as a non-woven bag supplier serving the Cairo and Alexandria markets, with three product lines fed by one supplier.
- Kenya — shopping bag manufacturer supplying supermarket chains. Three units (ZXL-A700 ×2, ZXH-C41200 ×1) produce branded non-woven shopping bags for nationwide supermarket chains and now supply more than 200 retail stores. The fully automatic line from printing to finished bag is managed by a single operator.
- Indonesia — large-scale non-woven bag manufacturing group. A 42-unit fleet spanning five machine models, including twelve ZXH-A1200 printing machines, built multi-line integrated production covering retail chain shopping bags, multi-color promotional bags, food-grade takeaway packaging and garment dust covers. The group supplies over one million bags monthly to major retail chains and food delivery platforms, and replaced imported bags from China with in-country production.
- Tanzania — promotional bag producer and corporate gift supplier. Two units (ZXL-A700Ultra ×1 plus ZXH-C21200 ×1) produce custom multi-color printed tote bags for corporate events, political campaigns and brand promotions. The business expanded from one to two production lines within 18 months and handles 10+ custom orders per week, which is exactly the changeover speed a quick-recall recipe system is specified for.
- Brazil — mid-scale manufacturer and packaging supplier. Six units across four machine types run supermarket shopping bags and breathable produce packaging bags for fruit and coffee exporters. A single equipment supplier covered four bag types, with unified after-sales support and interchangeable spare parts across models.
Comparison: ZXH Printing Models and Automation Tiers
Buyers comparing a non woven bag printing machine usually compare color count first. The specification data below is the part that determines whether that color count can actually be produced at the required output.
| Model | Printing type | Colors | Max fabric roll width | Max printing size / width | Printing length | Plate thickness | Printing speed | Total power | Weight |
|---|---|---|---|---|---|---|---|---|---|
| ZXH-A1200 | Screen | 1 color | 1,250 mm | 1,100 × 1,200 mm | — | — | 1,500–4,000 m/hour | 26 kW | 4,800 kg |
| ZXH-B1200 | Screen | 2 color | 1,250 mm | 1,100 × 1,200 mm | — | — | 1,500–3,000 m/hour | 52 kW | 9,600 kg |
| ZXH-C21200 | Flexo | 2 color | 1,200 mm | Max printing width 1,160 mm | 250–1,000 mm | 2.28 / 3.94 mm | 10–60 m/min | 8 kW | 1,500 kg |
| ZXH-C41200 | Flexo | 4 color | 1,200 mm | Max printing width 1,160 mm | 220–1,000 mm | 2.28 / 3.94 mm | 10–60 m/min | 18 kW | 3,000 kg |
Two observations follow from the table. First, screen printing models cover large single- or two-color formats and high linear speeds, while flexo models cover multi-color work with a defined printing length range — the choice follows the artwork, not the price list. Second, power draw and machine weight scale with color count and format, which means floor loading, electrical capacity and compressed-air sizing have to be planned at specification stage, not after delivery.
| Specification point | Fully automatic inline | Semi-automatic |
|---|---|---|
| Output speed | 100–120 pcs/min | 15–20 pcs/min |
| Operators | 1 operator per 2 machines | 3–4 workers per line |
| Defect rate | Below 0.5% | 3–5% |
| Process flow | Integrated inline: feeding → printing → forming → sealing → cutting → counting → stacking | Separate stations with manual transfer between processes |
| Quality control | PLC self-diagnosis and preventive maintenance alerts | Constant mechanical adjustment required |
| Best fit | Supermarket chain and large retail supply, contract volumes with delivery penalties | Startups below roughly 10,000 bags/day, very small custom batches |
FAQ: Servo, PLC, Sealing and Purchasing Questions
1. Which certifications should be verified before ordering a non woven bag printing machine?
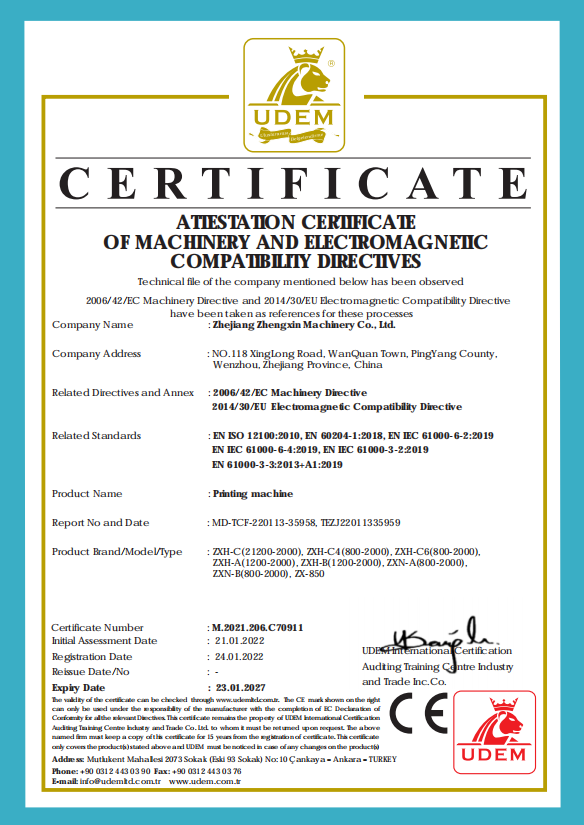
Two documents matter most. First, CE marking: the non woven printing machine models ZXH-C(21200-2000), ZXH-C4(800-2000), ZXH-C6(800-2000), ZXH-A(1200-2000), ZXH-B(1200-2000), ZXN-A(800-2000), ZXN-B(800-2000) and ZX-850 fall within a CE certificate issued by UDEM under certificate number M.2021.206.C70911, valid from 2022-01-24 to 2027-01-23, assessed against EN ISO 12100:2010, EN 60204-1:2018, EN IEC 61000-6-2:2019, EN IEC 61000-6-4:2019, EN IEC 61000-3-2:2019 and EN 61000-3-3:2013+A1:2019. EN 1010-1:2004+A1:2010 is the harmonized European standard for the safety of printing and paper converting machines, so it is a reasonable reference point when reviewing a supplier’s safety documentation. Second, ISO 9001:2015 — certificate 20225Q21503R2M issued by QPC, valid to 2029-01-12 under GB/T19001-2016/ISO9001:2015, with a scope covering production and sales of bag making machines, slitting machines and non-woven printing machines. Verify certificate numbers and validity on the issuing body’s own website, and confirm that third-party pre-shipment inspection by SGS, Bureau Veritas or CCIC is permitted.
2. Can a manufacturer supply an OEM flexo non woven bag printing machine built to my specification?
Yes — OEM and ODM services are available, and the minimum order quantity is 1 unit, so a single custom-configured machine can be ordered without a volume commitment. Configurable items include voltage and power (220V, 380V, 415V or 440V, single-phase or three-phase), printing colors (1–6 color flexo printing, single-side or double-side), control system (PLC from Siemens, Mitsubishi or Delta with a multi-language HMI touch screen), automation level (semi-automatic through to fully automatic with automatic stacking and counting), optional modules such as gusset makers, hole punches, folding units and bundling, machine color and branding, and motor brand (Siemens, ABB, SEW or domestic Chinese premium brands). Customization adds 5–10 working days to the production schedule, and monthly manufacturing capacity is 40 units.
3. How is the machine tested before shipment, and what are the acceptance criteria?
Acceptance is defined as pre-shipment testing, with 100% testing and quality control at incoming material inspection, in-process checkpoints and a continuous full-load production test before packing. Where sealing quality is the concern, the acceptance test is specific: after any parameter change, produce 20 test bags and pull-test 5 by hand — the seal must tear the fabric, not peel apart at the weld line, and a uniform glossy weld line indicates correct amplitude. Mechanical verification includes the horn-to-anvil gap, which should measure approximately 0.3–0.5 mm at 70 GSM fabric and be even within 0.05 mm across the full horn width when checked with a feeler gauge. Payment terms are 30% deposit and 70% before shipment, delivery terms FOB or CIF, and third-party inspection can be arranged at the buyer’s request before the balance is released.
4. Can I validate print registration and seal quality on samples before committing to a full order?
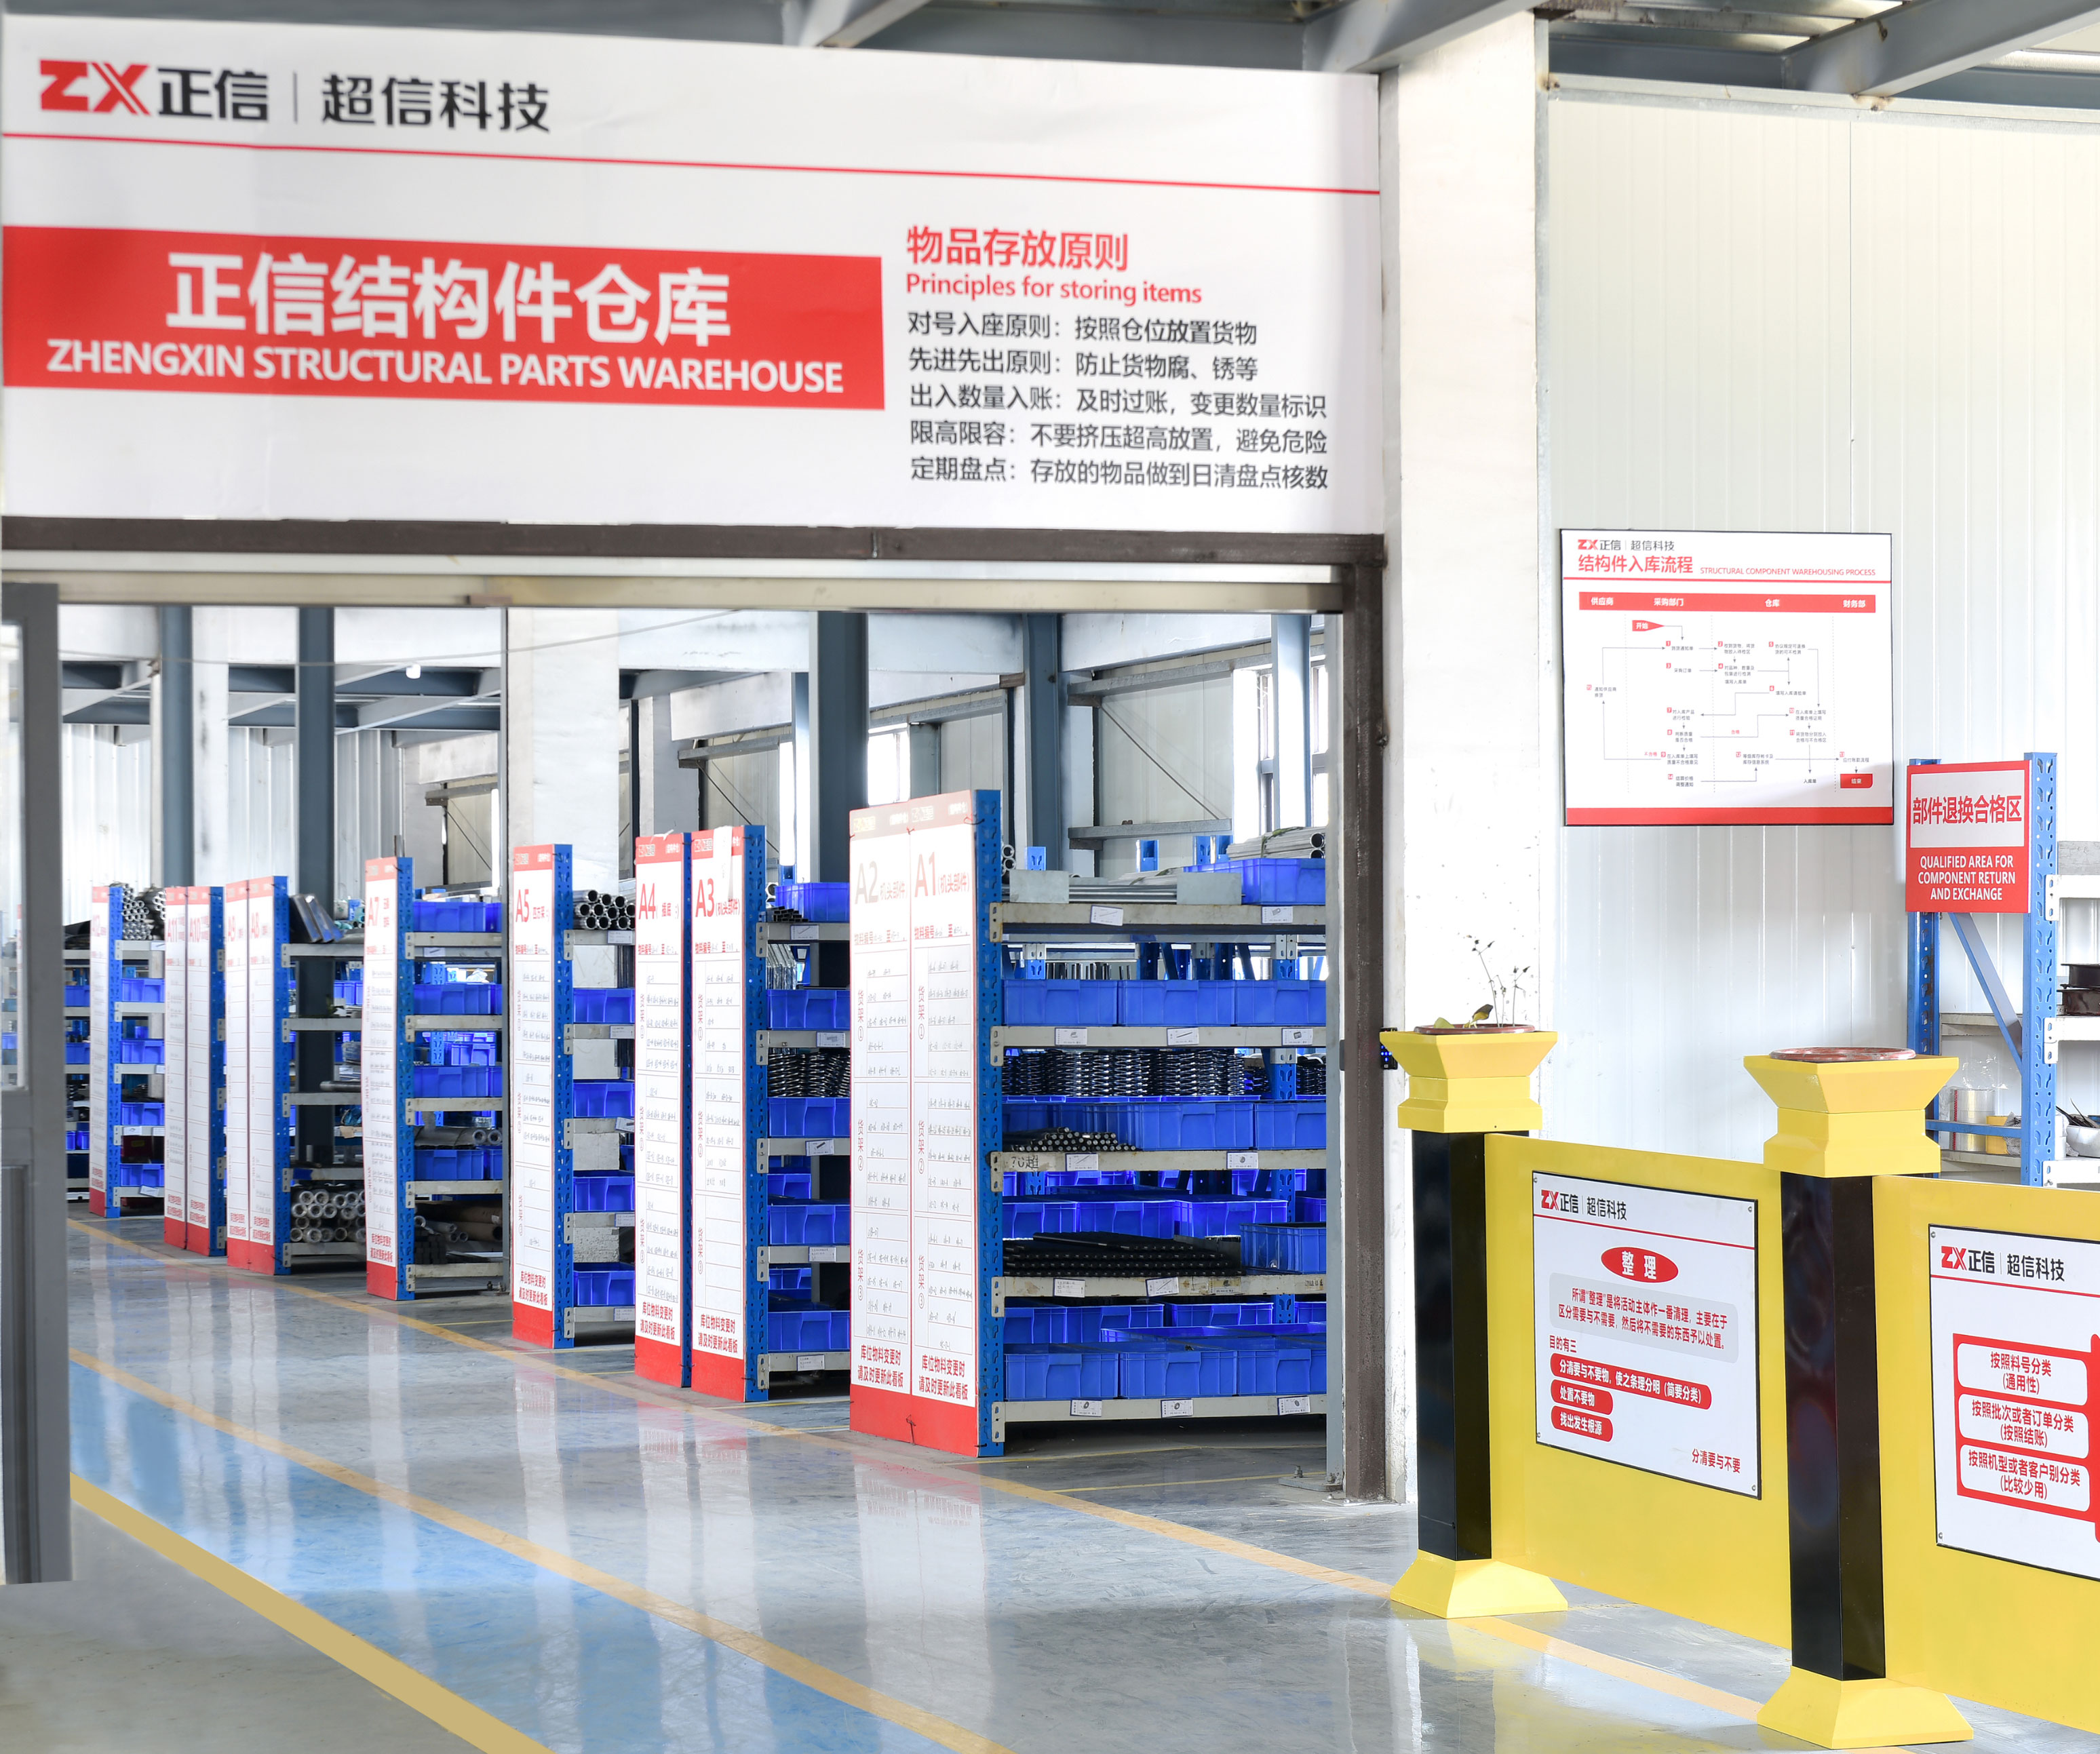
Sample validation is part of normal evaluation. Bag samples and print samples can be reviewed, a live video factory tour can be arranged showing production lines, testing areas, component inventory and machines under build — in real time rather than pre-recorded — and reference customers in the buyer’s region can be provided with their permission so performance, after-sales response and actual experience can be checked directly. This matters because registration quality depends on elements that are easier to verify on a sample than in a brochure: registration mark print consistency, photocell response and fabric tension stability across a full roll. Once installed, remote support is available seven days a week by WhatsApp and video call, and more than 80% of issues are diagnosed and resolved remotely.
5. What are the purchasing terms, lead time and next step?
Confirm five items in writing before ordering: minimum order quantity of 1 unit; delivery terms FOB or CIF; acceptance criteria defined as pre-shipment test; payment terms of 30% deposit and 70% before shipment; and production lead time, quoted in the 30–45 day range depending on configuration, with sea freight adding 15–45 days depending on destination. The machine ships with a one-year warranty on major components, installation and commissioning services, and access to on-site service by a professional team when remote diagnosis is not sufficient. Spare parts are dispatched by express courier, typically arriving within 3–7 days internationally. To move from specification to quotation, send your bag style, fabric GSM range, required color count and target daily output to the Zhengxin engineering team, and request a configuration sheet, sample review and pre-shipment inspection plan for the exact model.
Conclusion: Three Layers Decide the Outcome, Not the Color Count
A non woven bag printing machine is won or lost on three specification layers. The drive and control tier — servo drive with encoder feedback, a named PLC brand and a multi-language HMI with recipe storage — determines dimensional accuracy, energy consumption and how quickly a bag change can be executed. The integration level determines whether printing, forming, sealing, cutting, counting and stacking happen in one continuous flow at 100–120 pcs/min with one operator per two machines, or across separate stations at 15–20 pcs/min with three to four workers. Sealing reliability determines whether the output is sellable: method selection, amplitude and gap settings recorded per GSM, and a pull-test acceptance rule where the seal tears the fabric instead of peeling.
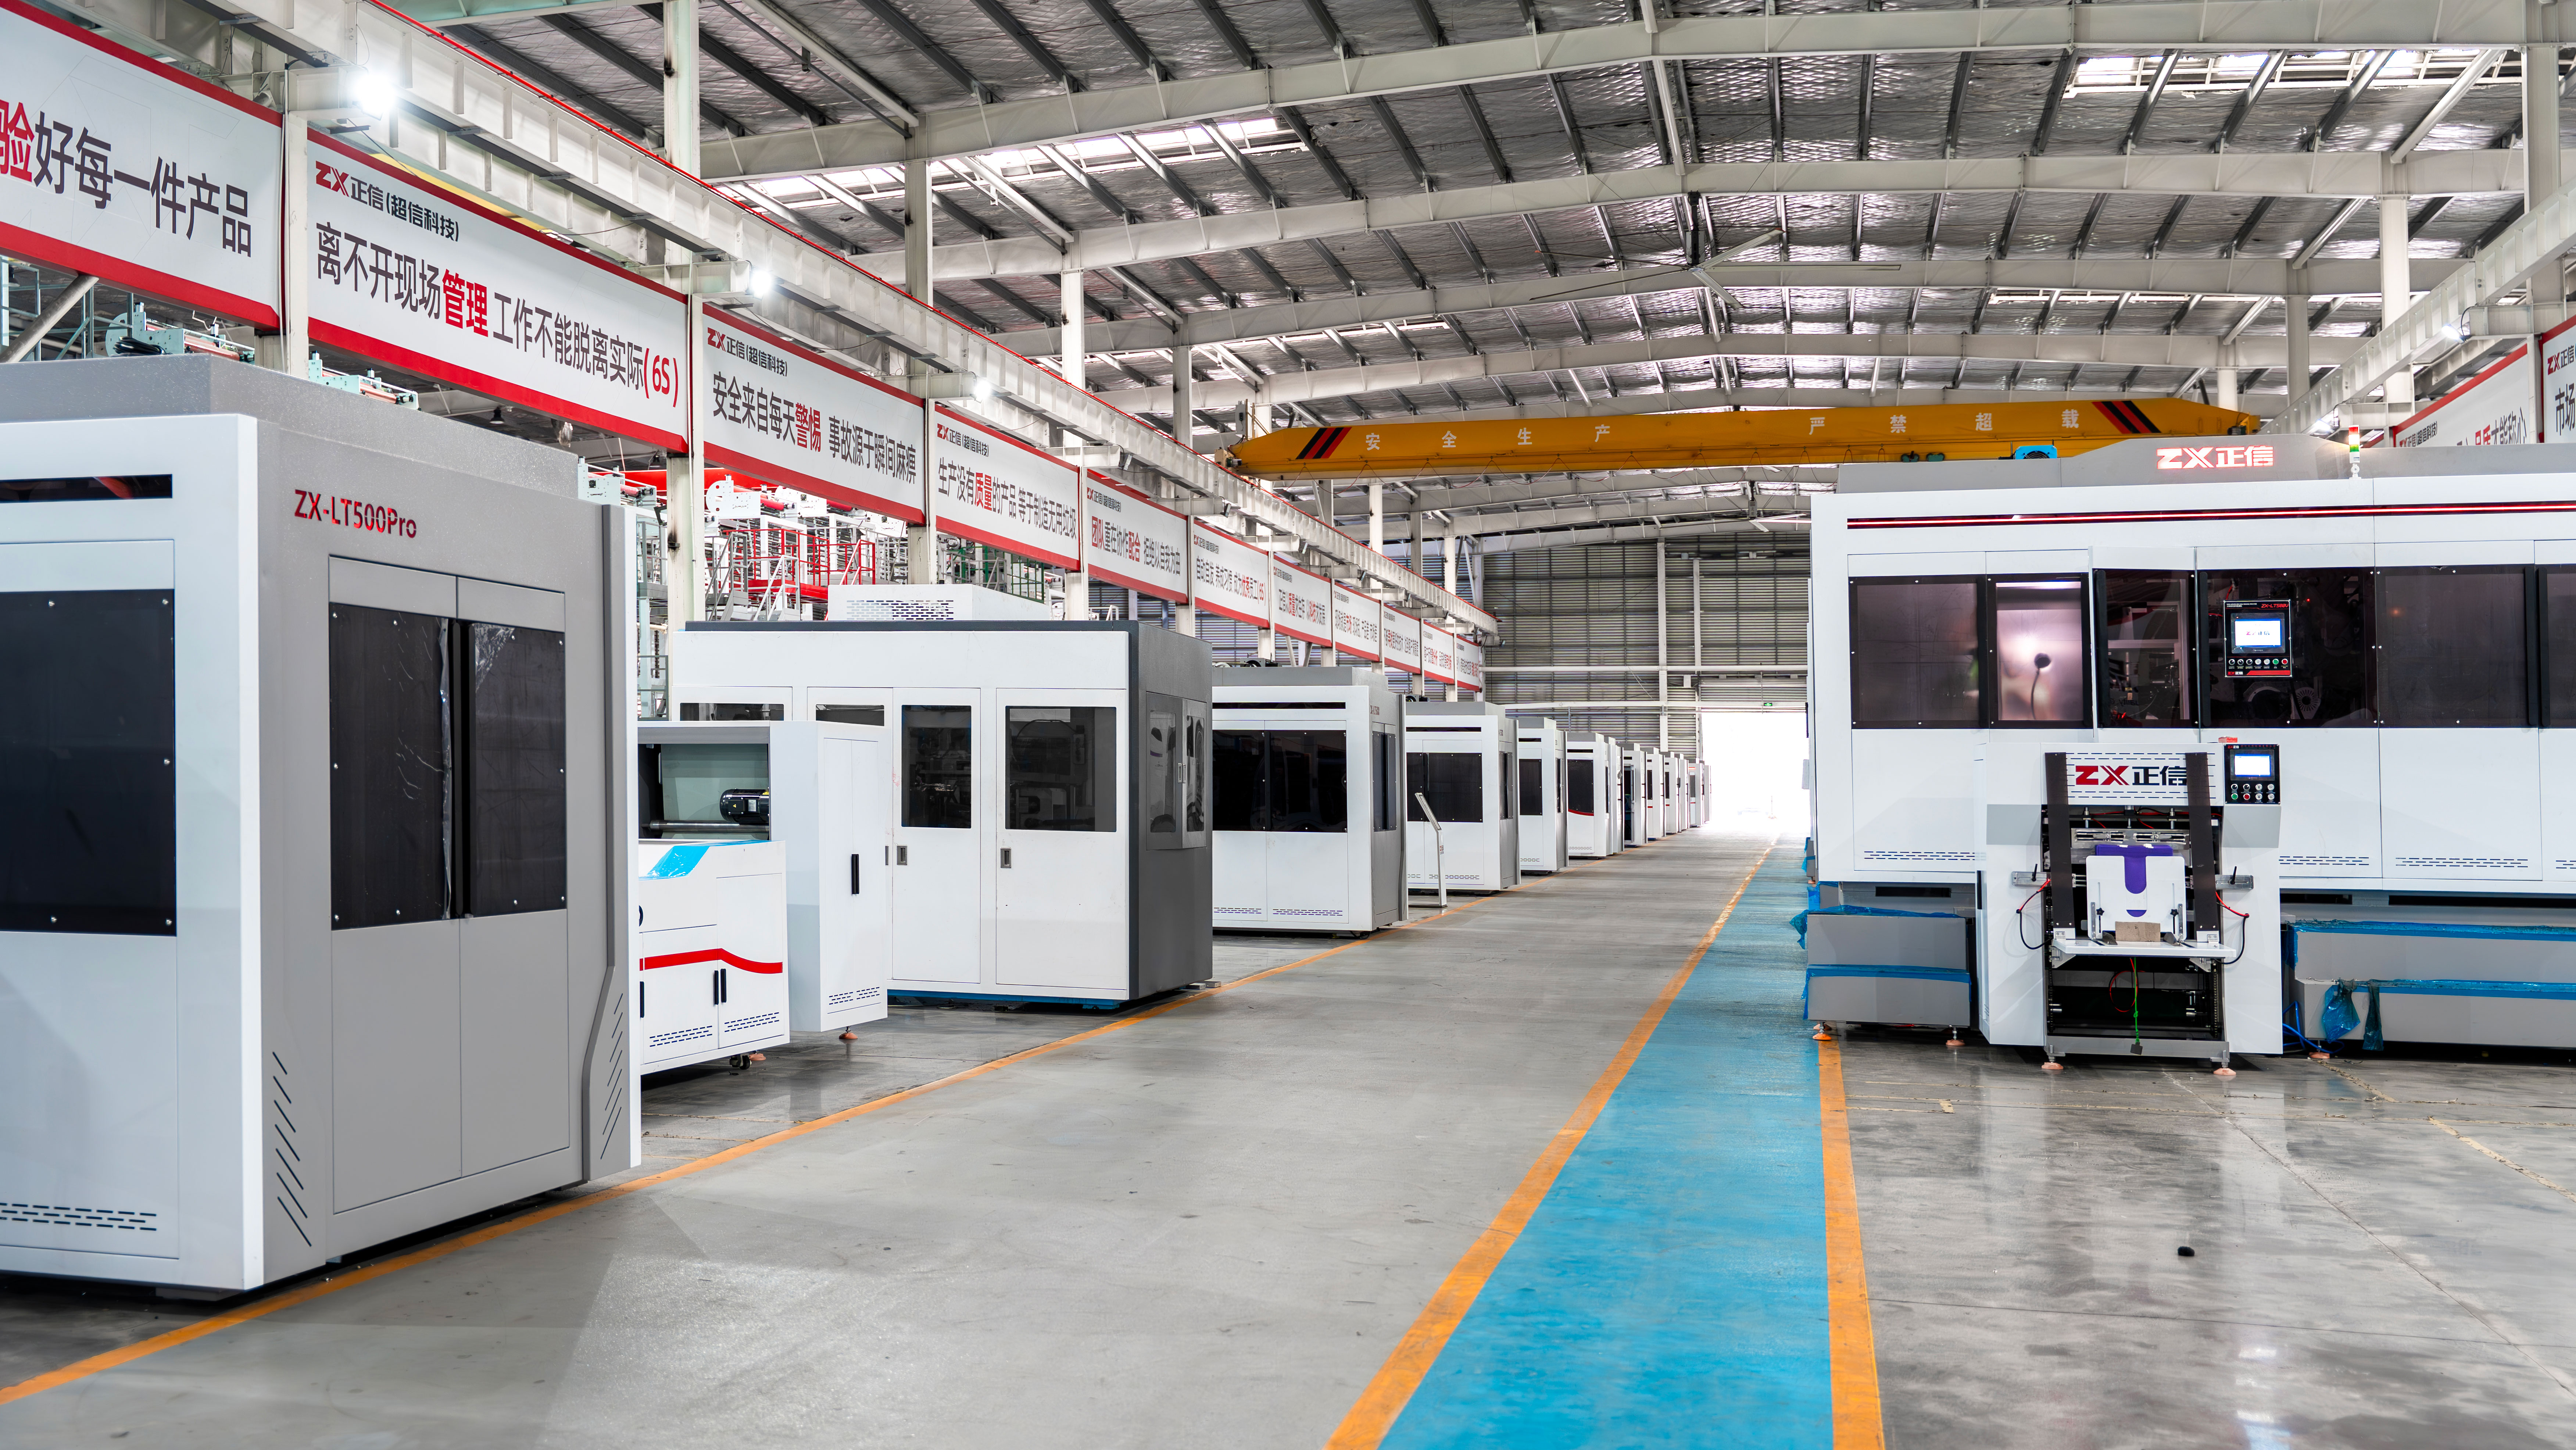
Zhejiang Zhengxin Machinery Co., Ltd. (ZX Zhengxin Machinery) is a manufacturer of non-woven bag making machines and complete non-woven bag production lines, headquartered in Wenzhou, Zhejiang. Founded in 2014, the company operates a 60,000 m² facility with 200 employees, a 30-engineer R&D team and an annual output of 500 units, exporting to over 120 countries with offices in Kenya, Morocco, Egypt, Vietnam, Tanzania, Dubai, Oman, Indonesia and Ethiopia. The product range covers non-woven bag making machines (ZXL series), flexo printing machines (ZXH series, 1–6 colors as customized), screen printing machines, 3D bag machines (ZX-LT500 series), fabric slitting machines (ZXC series) and supporting auxiliary equipment, built with genuine branded components and verified by third-party inspection on request.
Request a configuration sheet, sample review or quotation
Send your bag style, fabric GSM, required color count and target daily output, and the engineering team will return a model recommendation with the servo, PLC and sealing specification written out — plus an invitation to review sample bags or run a live factory video tour before you commit.
Website: www.wzzxjx.com | Blog: blog.wzzxjx.com
Email: info@zxcorp.com | Tel / WhatsApp: +86 158-5888-9595
WhatsApp: Start a conversation with an engineer
Address: No. 118 Xinglong Road, Wanquan Town, Pingyang County, Wenzhou City, Zhejiang Province, China
Download the full product catalogue: ZX Zhengxin Machinery 2026 Brochure (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.